In the production chain of new energy vehicle power battery ternary precursors (NCM), the extraction, separation, and deep purification of nickel, cobalt, and manganese are critical processes that determine the purity, electrochemical performance, and production cost of the final products. With the accelerating trend toward high-nickel materials, increasingly stringent impurity control requirements are being imposed on battery-grade nickel sulfate, cobalt sulfate, and manganese sulfate. Traditional extraction equipment has become increasingly difficult to meet the dual requirements of high-precision separation and large-scale continuous production.
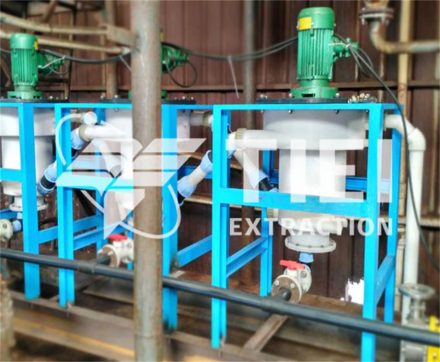
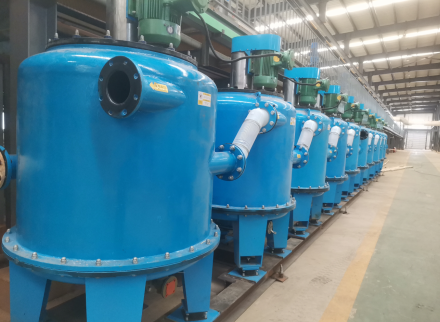
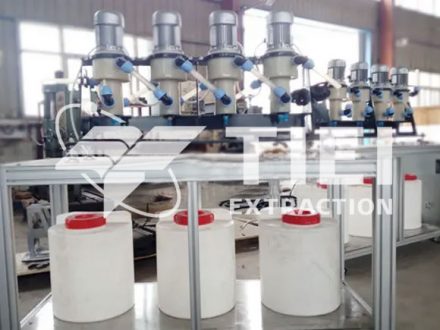
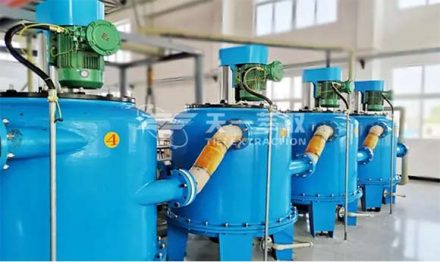
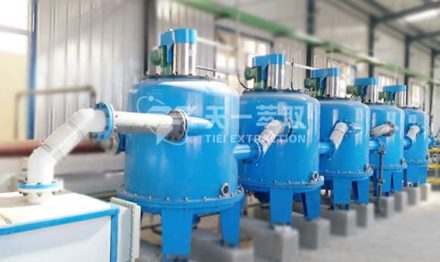
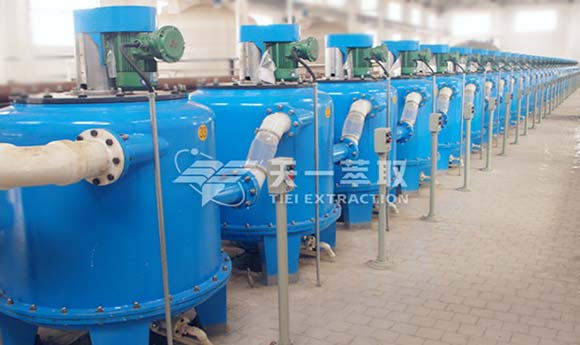
Tiei Extraction's CWL-M Series Centrifugal Extractor, featuring enhanced mass transfer and rapid phase separation technology, provide comprehensive equipment support throughout the entire process, from laboratory-scale research and development to industrial-scale production of nickel, cobalt, and manganese sulfate.
Challenges of Traditional Processes: Nickel, Cobalt and Manganese Separation Is Far More Difficult Than Single-Metal Systems
Nickel, cobalt, and manganese are all transition metals with similar ionic radii and chemical properties. In particular, the separation factor between nickel and cobalt is relatively low. Traditional mixer-settler systems may require 20–30 stages to achieve effective separation, resulting in a large footprint and high solvent inventory. In addition, ternary feed solutions are often accompanied by impurities such as iron, aluminum, calcium, and magnesium, which can easily cause emulsification and further reduce separation efficiency. Traditional equipment also has a long phase-separation time, often taking tens of minutes, while serious organic-phase entrainment can lead to fluctuations in product purity and high solvent consumption.
CWL-M Centrifugal Extractor: A Comprehensive Breakthrough from Principle to Process
The CWL-M Centrifugal Extractor utilizes a centrifugal force field of 800–1200 G generated by high-speed rotation, enabling the aqueous and organic phases to complete micron-scale mixing and mass transfer, followed by forced separation, within seconds. Its core technical advantages are reflected in the following aspects:
1.Higher mass transfer efficiency, reducing the number of stages by more than 40%.
Under the centrifugal force field, forced mixing breaks the liquid phases into micron-sized droplets, increasing the mass-transfer interfacial area by 5–8 times compared with traditional equipment. The extraction efficiency per stage is ≥90%. Under the same separation requirements, the number of stages required for nickel-cobalt separation can be reduced from 24 stages in traditional systems to 10–12 stages, significantly reducing equipment investment and footprint.
2.Precise separation, compatible with multiple extractant systems.
For nickel-cobalt-manganese sulfate systems, the CWL-M centrifugal extractor can be flexibly combined with extractants such as P204 for impurity removal and manganese extraction, P507 for nickel-cobalt separation, and Cyanex 272 for nickel-magnesium separation, enabling gradient separation. Through multistage counter-current extraction, the nickel recovery rate can reach more than 98%, the cobalt recovery rate can reach more than 96%, and the manganese recovery rate can reach more than 92%, with product purity meeting battery-grade standards.
3.Second-level phase separation, effectively eliminating emulsification and entrainment.
The powerful centrifugal force enables the two phases to separate clearly within 1–2 seconds. The organic-phase entrainment rate is <0.1%, fundamentally suppressing the accumulation of emulsified layers and ensuring continuous and stable operation.
4.Fully enclosed and corrosion-resistant, suitable for demanding operating conditions.
The equipment's wetted parts can be manufactured from 316L stainless steel, duplex stainless steel, or fluoropolymer materials, providing resistance to high-concentration sulfate solutions as well as acidic and alkaline corrosion. The fully enclosed structure prevents solvent volatilization, improves the working environment, and meets environmental protection and safety requirements.
5.Continuous automation and easy scale-up.
The modular design supports flexible connection of multiple stages. Experimental data can be directly and linearly scaled up to industrial equipment. The PLC intelligent control system monitors parameters such as rotational speed and flow rate in real time, enabling 24-hour continuous unattended operation.
Comprehensive Equipment Portfolio: Seamless Connection from R&D to Mass Production
The CWL-M Series Centrifugal Extractor covers a complete range of products, including the laboratory-scale, pilot-scale, and industrial-scale. The laboratory model has a throughput of 5–50 L/h, suitable for exploring and optimizing process parameters at the small-scale testing stage. The pilot-scale model has a processing capacity of 500–1,000 L/h, supporting verification of continuous process stability. Industrial models offer a single-unit processing capacity of 2–60 m³/h, supporting large-scale production at capacities of more than 10,000 tons per year. The fluid-dynamic parameters of equipment at different scales are based on the same design principles, ensuring scale-up without loss of process performance.
Application Case
In a nickel-cobalt-manganese sulfate extraction and separation project for a ternary precursor manufacturer, CWL-M Centrifugal Extractors were adopted to replace the original mixer-settler system, achieving the following improvements:
The number of nickel-cobalt separation stages was reduced from 24 to 12, while the footprint was reduced by 65%.
The nickel recovery rate increased from 94.5% to 98.2%, and the cobalt recovery rate increased from 92% to 96.5%.
Extractant consumption was reduced by 35%, saving more than RMB 2 million in annual operating costs.
The resulting nickel sulfate and cobalt sulfate products both achieved battery-grade purity standards.
Efficient separation of nickel, cobalt, and manganese is the foundation for the quality of ternary precursor materials. With its core technologies of enhanced mass transfer via centrifugal force field, second-level phase separation, and fully enclosed continuous operation, Tiei Extraction's CWL-M Series Centrifugal Extractor provides efficient and stable core equipment for the production of battery-grade nickel, cobalt, and manganese salts. We provide one-stop services from laboratory-scale testing to industrial-scale equipment, using actual customer feed-solution test data to provide reliable evidence for project evaluation and equipment selection.
Email: sales@tieiextraction.com
Whatsapp: +86 19069612820