HMB, or β-hydroxy-β-methylbutyric acid, is an important raw material in the food additive and sports nutrition industries. During its production and purification, the efficient recovery of HMB from the aqueous phase is a key factor affecting product yield, purity, and solvent consumption. Ethyl acetate is commonly used for HMB aqueous-phase extraction because of its good solubility for free HMB acid, ease of recovery, and suitability for food-grade production.
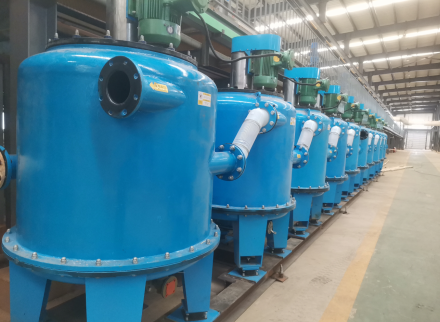
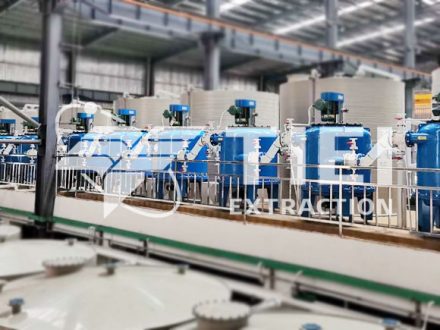
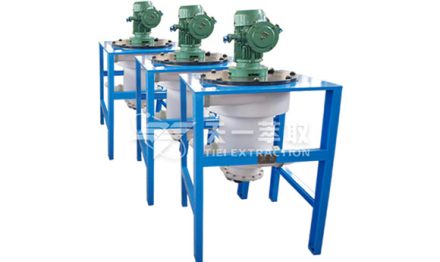
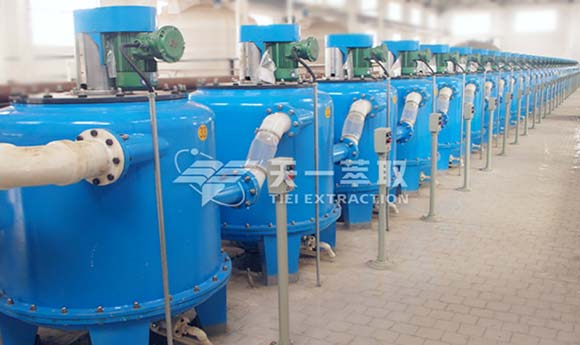
For continuous, large-scale production, four-stage countercurrent extraction combined with an organic-to-aqueous phase ratio (O:A) of 1.5:1 can achieve high extraction efficiency with relatively low solvent consumption. Zhengzhou Tiei Extraction specializes in liquid-liquid extraction equipment. Its CWL-M centrifugal extractor provides a continuous, enclosed, and efficient solution for HMB ethyl acetate extraction.
Why Choose Ethyl Acetate for HMB Extraction?
HMB may be present in the aqueous phase in the form of free acid or salt. When using ethyl acetate for extraction, the pH usually needs to be adjusted according to the condition of the feed solution to maintain HMB in its free acid form, which favors transfer into the organic phase. Ethyl acetate has a suitable density difference relative to the aqueous phase and good selectivity. The solvent can subsequently be recovered by distillation and recycled.
Food additive production requires stringent control of residual solvents, microbial contamination, and batch-to-batch consistency. Traditional mixer-settlers occupy large areas, may expose solvents to the environment, and typically operate intermittently. Extraction columns may have long residence times and be prone to backmixing. Centrifugal extractors use high-speed centrifugal separation to rapidly complete mass transfer during mixing and separate the two phases, making them more suitable for liquid-liquid extraction systems such as HMB that require continuous and stable process control.
HMB Extraction Process Flow
1.Aqueous-Phase Pretreatment
The HMB-containing aqueous phase may come from fermentation broth, reaction solution, or an intermediate purification stream. Suspended solids and some impurities are first removed by filtration, centrifugation, or decolorization. Depending on the existing form of HMB, the pH is adjusted to a range suitable for ethyl acetate extraction. The specific pH, temperature, and salt concentration should be determined through small-scale testing to avoid HMB degradation or excessive impurity transfer under extreme conditions.
2.Organic-Phase Preparation
Ethyl acetate is used as the extractant. Either fresh solvent or solvent recovered through distillation may be used. In food additive production, solvent purity must be controlled to prevent impurity accumulation from affecting product quality.
3.Four-stage Countercurrent extraction
Four CWL-M centrifugal extractors are connected in series. The aqueous phase enters at the first stage, and ethyl acetate enters at the fourth stage, with an O/A ratio of 1.5:1. Each stage performs mixing, mass transfer, and centrifugal separation, operating continuously in a four-stage countercurrent mode. The loaded organic phase exits from the first stage, while the raffinate aqueous phase exits from the fourth stage.
4.Back-extraction or Solvent Recovery
The loaded organic phase can be back-extracted with an alkaline aqueous solution to transfer HMB back into the aqueous phase, followed by concentration, crystallization, and drying to obtain the product. Alternatively, ethyl acetate can be recovered by distillation, followed by further purification of HMB. The recovered solvent is recycled to reduce operating costs.
5.Quality Control
The finished HMB product is tested for purity, moisture content, residual solvents, heavy metals, and microbial indicators in accordance with applicable food additive standards. Continuous, enclosed extraction helps reduce external contamination and solvent volatilization.
Advantages of the CWL-M Centrifugal Extractor in HMB Extraction
The CWL-M centrifugal extractor from Zhengzhou Tiei Extraction is suitable for HMB aqueous-phase–ethyl acetate extraction systems. Its main advantages include:
1.High-Efficiency Mass Transfer: The high-speed rotating drum ensures thorough mixing of the two phases and produces fine droplets, accelerating mass transfer.
2.Rapid Phase Separation: Separation occurs rapidly under a centrifugal force field, making the equipment suitable for systems that are prone to emulsification or have relatively small density differences.
3.Four-Stage Countercurrent Integration: Multiple stages can be flexibly connected in series, with precise control of the O:A ratio at 1.5:1 to support stable operation.
4.Enclosed, Continuous Operation: The enclosed design reduces ethyl acetate volatilization and occupational exposure, improving operational safety.
5.Small Footprint: Compared with traditional mixer-settlers, the modular design saves space and facilitates capacity expansion.
6.Sanitary Design: Options include 316L stainless steel and solvent-resistant sealing materials, with support for clean-in-place (CIP) cleaning.
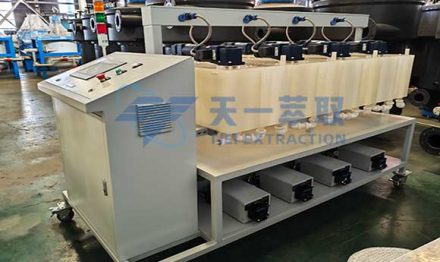
7.Automated Control: PLC-based control of flow rates, rotational speed, and interface conditions reduces manual intervention.
8.Reduced Solvent Consumption: Countercurrent extraction improves efficiency, reducing fresh solvent consumption and wastewater load.
Conclusion
As a food additive, HMB requires an aqueous-phase ethyl acetate extraction process that balances recovery yield, product purity, solvent recovery, and safety compliance. Four-stage countercurrent extraction at an O:A ratio of 1.5:1 can effectively improve HMB recovery efficiency while reducing solvent consumption. The CWL-M centrifugal extractor from Zhengzhou Tiei Extraction provides a continuous, enclosed, and efficient equipment solution for HMB liquid-liquid extraction, supporting small-scale testing, pilot-scale trials, and process scale-up.
For more information about HMB ethyl acetate extraction processes or CWL-M centrifugal extractor, please contact Zhengzhou Tiei Extraction.
Email: sales@tieiextraction.com
Whatsapp: +86 19069612820