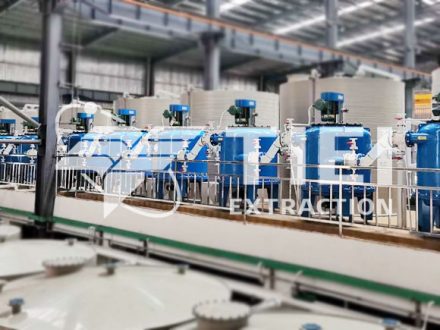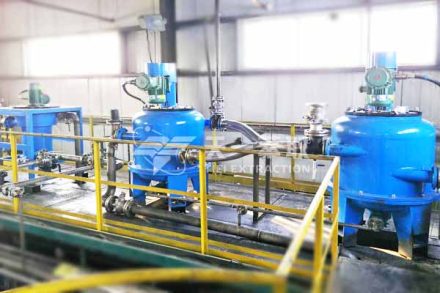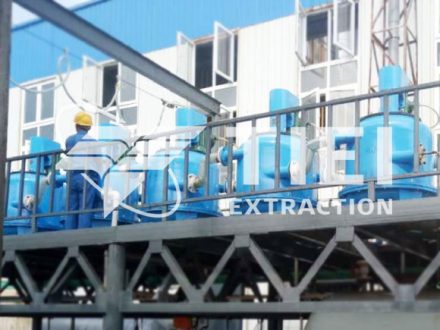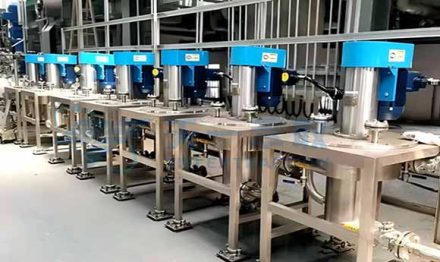
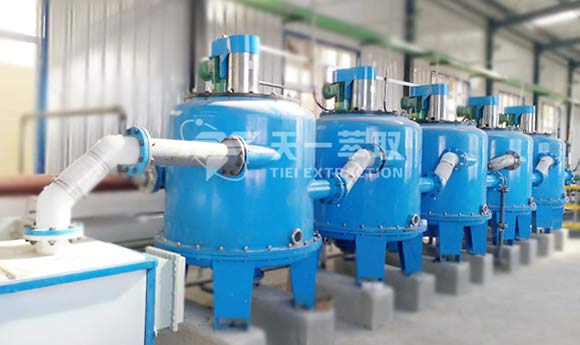
Nickel and cobalt are adjacent elements in the periodic table and share similar chemical properties. They almost always occur together in associated ores and secondary resources. For this reason, nickel-cobalt separation has long been recognized as a major challenge in hydrometallurgy. Chemical precipitation methods offer limited selectivity and often result in inconsistent product purity, and have gradually been replaced by solvent extraction. Within solvent extraction systems, the choice of equipment is becoming one of the key factors determining nickel-cobalt separation performance. The CWL-M centrifugal extractor from Zhengzhou Tiei Extraction is an industrial-grade liquid-liquid extraction equipment specifically designed to address this critical stage.
Core Process Flow of Nickel-Cobalt Solvent Extraction
Regardless of whether the feed material comes from nickel-cobalt ore leachate or spent lithium-ion battery recycling solutions, the main process flow for nickel-cobalt separation by solvent extraction remains the same: extraction—washing—stripping—regeneration.
During the extraction stage, the aqueous feed solution containing nickel and cobalt comes into full contact with a selective extractant (such as the P507 system) inside the centrifugal extractor, facilitating mass transfer. The extractant preferentially complexes with cobalt (or nickel, depending on the process design), forming a loaded organic phase, while the raffinate is discharged as a purified solution containing the target metal. Subsequently, the loaded organic phase enters the washing stage, where a washing solution of a specific concentration is used to remove co-extracted impurity metals. The washed loaded organic phase then enters the stripping stage, where stripping agents such as sulfuric acid transfer the target metal back into the aqueous phase, producing a high-concentration metal salt solution. The barren organic phase is regenerated and returned to the extraction stage for recycling.
In spent battery recycling solution systems, this process typically follows the sequence of "initial impurity removal—cobalt extraction—nickel extraction—washing—stripping—regeneration." The number of extraction stages and the organic-to-aqueous phase ratio (O/A) are adjusted according to the composition of the feed solution.
The key engineering challenge lies not in the process flow itself, but in the phase contact and separation speed at each stage. Mixer-settler systems rely on gravity for phase separation, requiring long residence times and large liquid-holding volumes. They also have limited adaptability to easily emulsified systems and feed solutions containing suspended solids. In contrast, centrifugal extractors use centrifugal force instead of gravity to achieve phase separation, reducing separation time from minutes to seconds and making stable, continuous operation.
Technical Positioning of the CWL-M Centrifugal Extractor in Nickel-Cobalt Extraction Processes
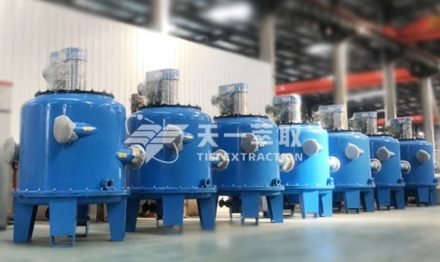
The CWL-M series centrifugal extractor is a fourth-generation product developed by Zhengzhou Tiei Extraction to address the structural limitations of traditional annular-gap centrifugal extractors. Its suitability for nickel-cobalt extraction processes is primarily based on three fundamental design features.
1.No bottom bearing and no risk of shaft seal leakage
Traditional centrifugal extractors are equipped with bearings and seals at the bottom of the rotating drum. When exposed to strong acids, strong alkalis, and organic solvents, these components present significant risks of corrosion and leakage. The CWL-M centrifugal extractor eliminates the bottom bearing and shaft seal structures, removing these potential failure points at the source and significantly reducing downtime and safety risks caused by equipment leakage in nickel-cobalt extraction operations.
2.Short residence time at each stage, suitable for easily emulsified systems
Nickel-cobalt extraction feed solutions often contain small amounts of suspended solids or surface-active substances, which can easily form stable emulsion layers in mixer-settler systems. The high-speed centrifugal separation of the CWL-M centrifugal extractor enables the two phases to complete mixing and separation within an extremely short residence time, reducing the conditions that lead to emulsion accumulation. Its tolerance to feed solutions containing suspended solids and interfacial contaminants is significantly better than that of gravity-based separation equipment.
3.Structurally reduced power consumption
Under the same processing capacity, the power consumption of the CWL-M centrifugal extractor is only 10%–30% of that of traditional annular-gap models. For nickel-cobalt extraction processes involving multiple stages connected in series and 24-hour continuous operation, the cumulative difference in electricity consumption is a significant factor in operating costs.
Key Advantages of the CWL-M Centrifugal Extractor for Nickel-Cobalt Separation
1.Single-stage extraction efficiency exceeds 95%, reducing the required number of stages
The CWL-M centrifugal extractor uses the centrifugal force field generated by the high-speed rotation of its drum to intensify two-phase mixing and mass transfer. Its single-stage extraction efficiency can reach over 95%. In nickel-cobalt separation, higher single-stage efficiency means that fewer stages connected in series are required to achieve the same separation depth, directly reducing the number of equipment units, floor space requirements, and the complexity of interstage piping. Comparative studies with mixer-settlers have also shown that centrifugal extractors require a lower organic-to-aqueous phase ratio (O/A) and shorter equilibrium time to achieve the same extraction rate, while significantly reducing organic phase entrainment in the raffinate.
2.Processing capacity covers the full range from laboratory testing to industrial-scale production
The smallest model in the CWL-M series centrifugal extractors, the CWL25-M, can be used for laboratory-scale testing and multi-stage counter-current simulation, while larger models such as the CWL650-M and CWL900-M are directly suited to industrial-scale nickel-cobalt extraction production lines. Using the same technology platform from process validation to scale-up reduces the uncertainties associated with scale-up effects.
3.Lower solvent consumption and entrainment losses
Rapid centrifugal phase separation ensures thorough separation of two phases, keeping the amount of organic phase entrained in the aqueous phase at a relatively low level. In actual operation, this characteristic translates into a 30%–40% reduction in solvent consumption, along with a corresponding reduction in the workload of the stripping and regeneration stages. For nickel-cobalt projects where extractant costs account for a significant proportion of operating expenses, every reduction in solvent loss directly contributes to improved economic performance.
4.Corrosion-resistant construction and continuous operation
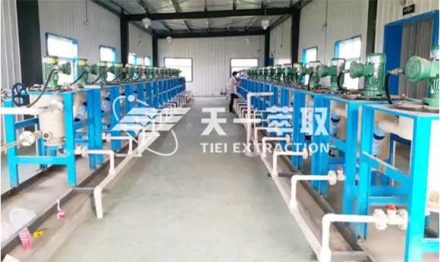
The main body of the CWL-M centrifugal extractor is made of 316L stainless steel, and its sealing system is configured to withstand environments involving strong acids, strong alkalis, and organic solvents. It supports the typical operating conditions of nickel-cobalt extraction processes, including high-acidity stripping and saponification operations. Its modular multi-stage series-connected design allows the extraction, washing, and stripping sections to be flexibly configured according to the required process stages, enabling continuous operation throughout the entire process rather than relying on batch switching.
Zhengzhou Tiei Extraction can provide CWL-M centrifugal extractor model selection and multi-stage series-connected process configuration solutions based on feed characteristics (ore leachate, battery dismantling solutions, or feed solutions containing impurities), processing capacity, and separation objectives. We also support centrifugal extraction testing and validation at laboratory and pilot scales. For process discussions concerning specific nickel-cobalt feed solutions or equipment technical specifications, please feel free to contact Tiei Extraction.
Email: sales@tieiextraction.com
Whatsapp: +86 19069612820